Featured Flexible OEM Puree Pouch Solutions
Engineered with High-Barrier Lamination, Anti-Choke Caps, and Cold-Chain / Retort Compatibility for Global and Panama Distribution
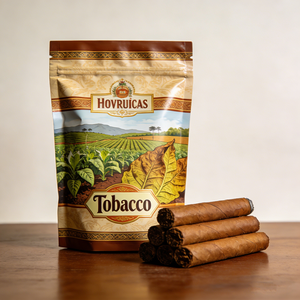
Custom Gravure Printed Foil Stand-Up Spout Pouch
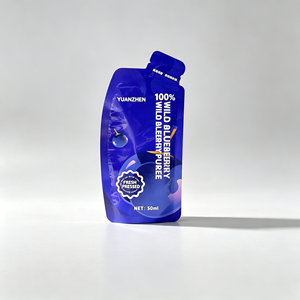
50ml Custom Irregular Blueberry Puree Beverage Pouch
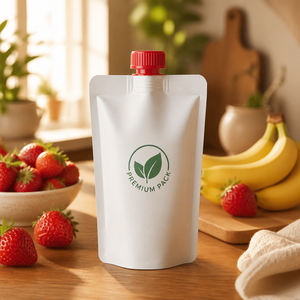
120g Organic Baby Food Spout Pouch with Anti-Choke Cap
3oz/4oz/5oz Stand-Up Puree & Juice Foil Spout Bag
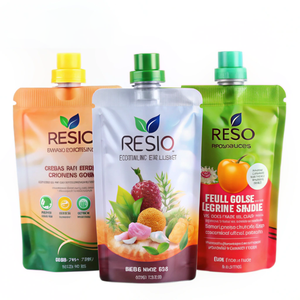
150ml-300ml High-Temperature Retort Puree Doypack
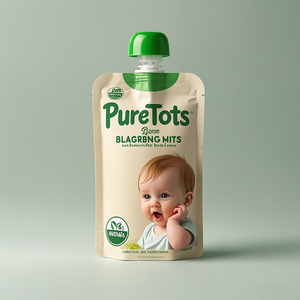
100ml-250ml Baby Nutrition Fruit Puree Spout Pouch
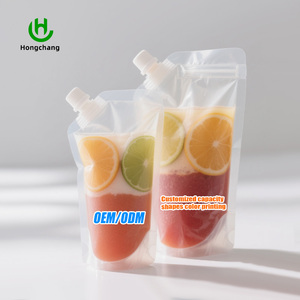
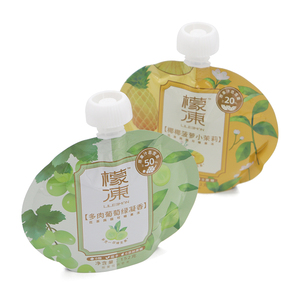
Moisture-Resistant Liquid & Puree Doypack Packaging
Panama Flexible Packaging Market Overview: Strategic Gateway for Puree Distribution
Panama occupies a unique position in global trade. Serving as the primary logistics backbone of Central America and the Caribbean via the Panama Canal, the Zona Libre de Colón (Colón Free Trade Zone), and Pacific/Atlantic port terminals, Panamanian food brands, co-packers, and distributors require flexible packaging solutions that perform seamlessly across tropical domestic climates and rigorous international re-export routes.
The demand for custom OEM puree pouches in Panama has experienced exponential growth. Driven by expanding domestic fruit processing sectors—particularly tropical puree production including passion fruit (maracuyá), mango, soursop (guanábana), papaya, and banana—alongside an surging market for organic baby nutrition and functional wellness gels, flexible squeeze pouches have rapidly replaced glass jars and rigid tin cans.
Why Panamanian Processors Prefer Spout Pouches over Traditional Glass and Cans:
Flexible stand-up spout pouches (Doypacks) deliver significant operational efficiencies across Panama's supply chain:
- 85% Tare Weight Reduction: Unfilled spout pouches weigh up to 85% less than glass jars, dramatically lowering freight transport costs from manufacturing facilities in Panama City and Chiriquí to distribution centers.
- Optimized Container Loading: Flexible pouches utilize up to 95% of shipping volume, whereas rigid glass containers waste crucial cubic capacity on empty space and protective corrugated dividers.
- Thermal Retort Efficiency: Thin flexible laminate profiles allow faster thermal penetration during hot-fill or retort sterilization process cycles (121°C), preserving natural flavors, vibrant tropical fruit colors, and delicate vitamins.
- Consumer Convenience: Resealable anti-choke choke-proof spouts cater directly to modern, active lifestyles, allowing effortless squeeze dispensing for baby food, sports nutrition, and culinary fruit purees on the go.
Engineering & Manufacturing Excellence for Puree Packaging
Precision-Crafted Material Formulations Tailored for Tropical Stability and Sterilization
High-Barrier Lamination
Engineered multi-layer structures (PET/AL/NY/PE or PET/EVOH/PE) providing zero light transmission, low oxygen permeability (<0.1 cc/m²/24h), and superior water vapor barriers (<0.1 g/m²/24h).
Anti-Choke Safety Caps
Child-safe, large-diameter anti-swallow caps compliant with international pediatric safety regulations (FDA, EU 10/2011). Prevents accidental ingestion hazards in infant baby food puree lines.
121°C Retort Thermal Stability
Specialized cast polypropylene (CPP) seal layers and aliphatic adhesives withstand high-pressure steam retort processing up to 121°C for 30 minutes without seal degradation or pouch bursting.
10-Color Rotogravure Printing
High-definition photo-realistic graphic reproduction using eco-friendly solvent-free inks. Matte, gloss, metallic hologram, and tactile registration effects to maximize shelf appeal in retail stores.
100% Hermetic Seal Integrity
Automated ultrasonic and heat-seal spout insertion technologies guarantee leak-proof corner or center spout seals. Burst test verified to exceed 180 kPa internal hydraulic pressure.
Custom Die-Cut Ergonomic Shapes
Precision die-cut profiles designed for comfortable handheld squeezing by infants and children, featuring smooth rounded safety corners to prevent scratches or accidental injuries.
Localized Packaging Application Scenarios in Panama
Understanding regional commercial environments is critical to engineering the correct pouch specifications. We supply custom OEM puree pouches across four primary operational sectors in Panama:
1. Chiriquí Agricultural Belt: Tropical Fruit Puree & Concentrate Exports
Panama's fertile highlands in Chiriquí, alongside agricultural zones in Azuero and Coclé, produce world-class tropical crops. Local processors converting fresh mango, passion fruit, papaya, and soursop into bulk and retail purees require reliable packaging to export across Central America, North America, and Europe. Our aluminum-foil laminated 200ml to 500ml stand-up spout pouches protect fresh fruit flavors against oxygen oxidation and thermal degradation, enabling ambient shelf storage of up to 18 months.
2. Colón Free Trade Zone (Zona Libre de Colón) Re-Export Packaging
As the largest free trade zone in the Western Hemisphere, Colón serves as the distribution nerve center for multinational consumer packaged goods (CPG) companies re-exporting to Colombia, Ecuador, Central America, and the Caribbean islands. We provide private-label OEM brands with standardized, multi-lingual printed pouches (Spanish, English, French, Portuguese) compliant with LATAM labeling laws, shipped in ultra-durable palletized packaging ready for rapid transshipment.
3. Panama City Retail & Modern Urban Supermarkets
Panama City boasts a highly sophisticated retail landscape (Riba Smith, Super 99, Rey, PriceSmart). Urban consumers increasingly demand organic baby food purees, dairy yogurt pouches, and low-glycemic fruit snacks packaged in modern squeeze formats. Our premium matte-finished pouches with custom transparent viewing windows allow consumers to inspect product purity, driving on-shelf conversion.
4. Sports Hydro-Gels & Eco-Tourism Hydration Pouches
Panama’s thriving sports, outdoor endurance, and eco-tourism markets (Bocas del Toro, Boquete, San Blas) require compact, lightweight, puncture-resistant 50ml to 100ml ergonomic squeeze pouches for energy gels, electrolyte purees, and liquid nutrition. Our high-tensile flexible materials withstand extreme outdoor compression without bursting.
Material Formulations & Technical Specifications
Compare Barrier Performance Attributes Across Our Popular OEM Puree Pouch Structures
| Structure Configuration | Material Lamination | Barrier Level | Primary Application | Processing Temperature |
|---|---|---|---|---|
| High-Barrier Foil (AL) | PET / AL / NY / CPP | Ultra-High (Light/O₂/Moisture) | Retort Baby Food & Shelf-Stable Purees | Retortable up to 121°C (250°F) |
| Transparent Barrier (EVOH) | PET / EVOH-PE or PET / NY / PE | High Oxygen & Moisture Barrier | Purees Requiring Product Visibility Window | Hot-Fill up to 85°C - 90°C |
| Metallized Economy (VMPET) | BOPP / VMPET / PE | Medium-High Moisture Barrier | Short Shelf-Life & Cold-Chain Beverages | Cold-Fill / Ambient Process |
| Eco Mono-Material (Recyclable) | MDO-PE / EVOH-PE / PE | High Barrier (Recycle Stream Code 4) | Sustainable Baby Food & Eco Purees | Warm-Fill up to 75°C |
Regulatory Trends & Sustainability Shifts in Panama Packaging
Panama has taken progressive legislative steps toward plastic waste reduction, highlighted by Law 187 (Ley 187), which regulates single-use plastic articles and mandates eco-conscious packaging alternatives across commercial sectors. As a forward-thinking OEM/ODM manufacturer, we assist Panamanian food brands in navigating regulatory compliance through advanced packaging engineering:
Transition to Mono-Material Recyclable Puree Pouches
Traditionally, high-barrier puree pouches incorporated mixed material layers (e.g., PET bonded to Aluminum and PE), making mechanical recycling impossible. To address Panama's circular economy goals, we have engineered 100% Mono-PE (Polyethylene) recyclable spout pouches. By pairing MDO-PE (Machine Direction Oriented PE) outer printing layers with EVOH-PE barrier sealants, our mono-material pouches deliver identical oxygen and moisture protection while fitting directly into Code 4 PE recycling streams.
BPA-Free, Phthalate-Free, & Food Safety Certifications
Food contact safety is non-negotiable, particularly for infant nutrition. All raw resin materials, spout fitments, color masterbatches, and laminating adhesives utilized in our facilities comply strictly with global safety standards:
- FDA 21 CFR 177.1520: Olefin polymers for direct food contact.
- EU Commission Regulation (EU) No 10/2011: Plastic materials intended to come into contact with food.
- Heavy Metals & Phthalates: Fully certified compliant with CONEG and EU REACH directives.
Why Partner with Us for Your OEM Production in Panama
End-to-End OEM/ODM Manufacturing Capabilities Backed by International Quality Standards
Global Quality Audit Standards
Our manufacturing sites operate under strict IFS Food, BRCGS Grade A+, HACCP, and ISO 22000 certified quality management systems, ensuring seamless audit approvals for Panama imports.
Fully Automated Spout Assembly
High-speed automatic spout heat-sealing machinery ensures zero thermal distortion around spout bases, guaranteeing consistent seal strength across millions of units.
Panama Logistics Coordination
Direct ocean shipping routes to Balboa (Pacific) and Manzanillo / Colón Container Terminal (Atlantic). Complete export documentation including Certificates of Analysis (COA) and Sanitary Declarations.