Featured OEM/ODM Gluten-Free & Snack Formulations
Customizable B2B snack solutions produced in state-of-the-art facilities compliant with IFS, BRCGS, Halal, and ISO standards.
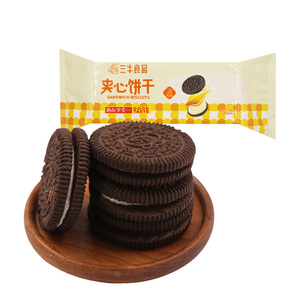
Sanniu Sweet Sandwich Biscuits Box 300g Healthy Snacks
Send an Inquiry
Top Trusted Gluten Free Factories & Factory: Strategic B2B Sourcing Guide
The global demand for gluten-free snacks and clean-label foods has undergone a structural shift. What was once a niche clinical market serving celiac patients has expanded into a mainstream wellness industry valued at tens of billions of dollars globally. For institutional buyers, procurement directors, brand owners, and wholesale distributors, securing a partnership with a certified gluten-free factory is no longer merely about product supply—it is a critical exercise in risk mitigation, allergen control engineering, and brand equity protection.
Navigating the competitive ecosystem of contract manufacturing requires rigorous evaluation of factory infrastructures. A genuine gluten-free food production facility must go far beyond marketing claims; it requires dedicated air handling units (HVAC), strictly segregated raw material intake zones, automated cleaning-in-place (CIP) protocols, and quantitative testing mechanisms capable of consistently verifying gluten concentrations well below international statutory caps (<20 ppm according to Codex Alimentarius, FDA, and EU Regulation No 828/2014).
Core Engineering Pillars of Reliable OEM Manufacturing
How top-tier food processing plants safeguard product purity while maintaining maximum volumetric output.
Zero-Cross Contamination Architecture
Physically separated production halls, dedicated processing machinery, and isolated air purification loops ensure wheat, rye, and barley proteins never enter certified zones.
ELISA & PCR Lab Validation
On-site ISO 17025 accredited quality control laboratories running daily R5 ELISA assays and PCR testing to verify gluten levels remain reliably below 5 ppm before batch clearance.
Global Accreditation Suite
Fully certified under IFS Food (Higher Level), BRCGS (Grade AA), HACCP, Halal, Kosher, and USDA Organic standards, streamlining global customs import approval.
Automated High-Speed Packaging
Multi-head weighers, automated pouch-filling doypack lines, and protective nitrogen flushing technology designed to maximize shelf-life stability and moisture barrier integrity.
In-House R&D Customization
Expert food technologists specializing in starch rheology, alternative flour matrices (cassava, almond, rice, chickpea), and natural sugar replacement without sacrificing texture or crunch.
Advanced Manufacturing Plant Infrastructure
Our strategic production hubs feature over 18 dedicated processing lines designed to accommodate diverse snack formats ranging from extruded potato chips, crisp prawn crackers, and sandwich biscuits to functional gummies, jerky, and roasted nut packs.
By managing the complete lifecycle—from raw ingredient sourcing and enzymatic grain modification to custom secondary display packaging—our facility provides brand owners with an end-to-end private label manufacturing solution. This integrated operational structure reduces lead times to 45–60 days while delivering full lot-level supply chain traceability.
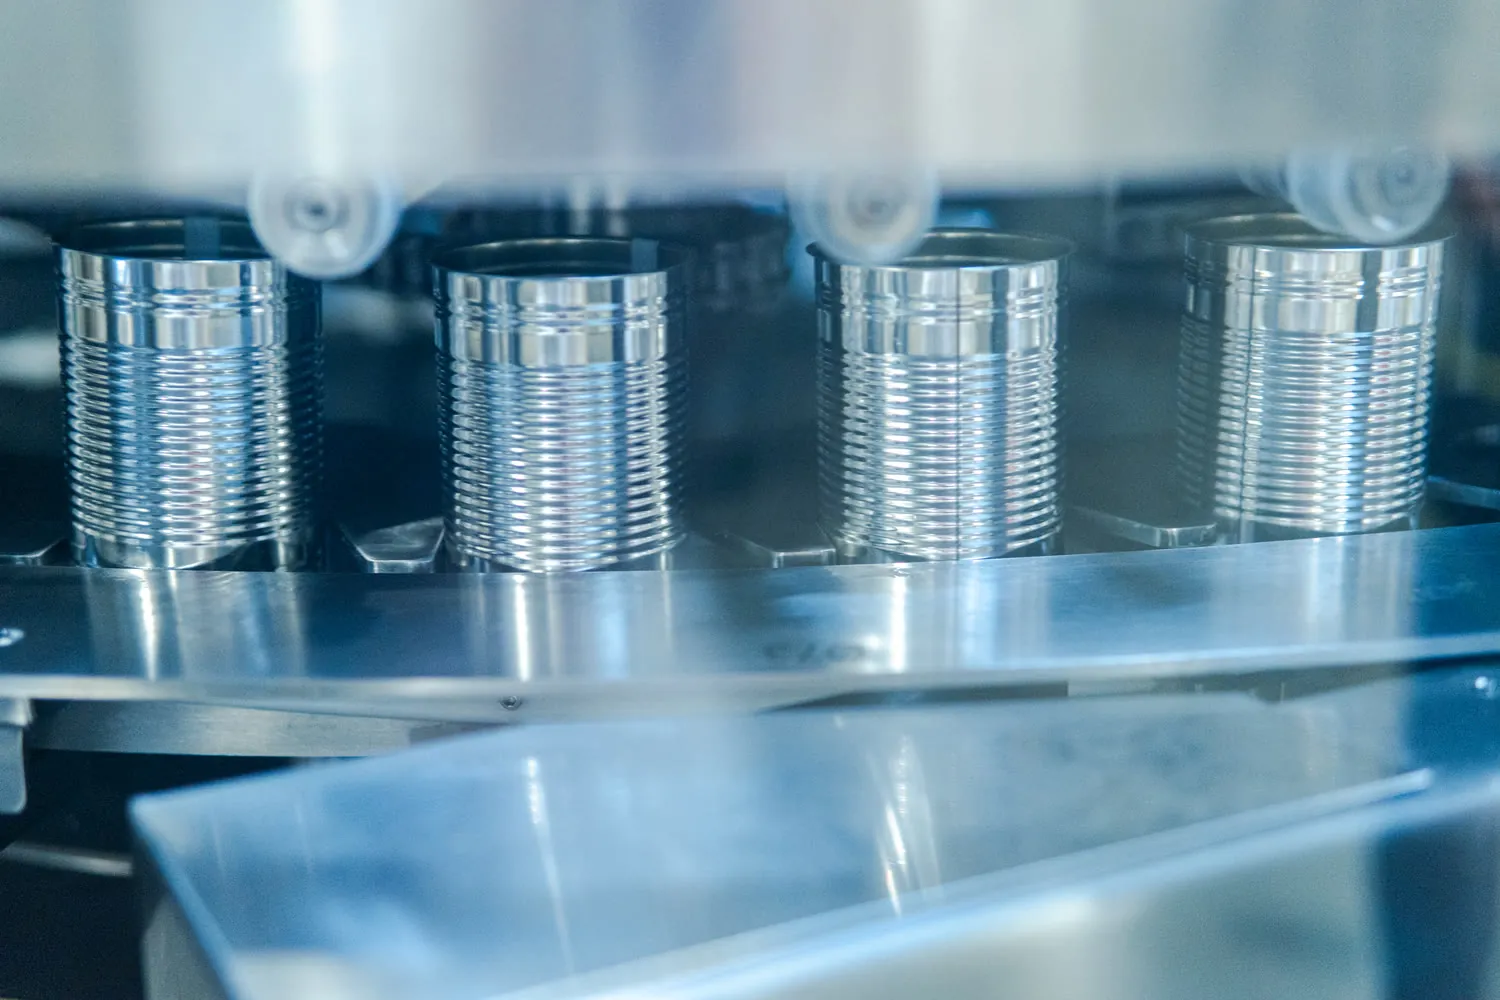
Engineering Cleanroom Standard Protocol in Gluten-Free Biscuit & Snack Production
When selecting a contract manufacturing partner, enterprise procurement teams must dissect the technical nuances of allergen isolation. Gluten proteins (gliadin and glutenin) possess high thermal stability and adhesive qualities, making complete removal from shared manufacturing lines exceptionally difficult without industrial-grade CIP (Clean-in-Place) systems and chemical sanitation cycles.
Leading facilities employ a three-tier preventative cross-contamination matrix:
- 1. Raw Material Supplier Auditing: Micro-milling flour facilities supplying tapioca, sorghum, or brown rice starches must submit batch-specific certificates of analysis (CoA) verified by third-party ELISA assays prior to warehouse receipt.
- 2. Zoning and Positive Air Pressure Controls: Production suites are segmented into strict hygienic zones. Processing rooms for free-flowing powders operate under controlled differential pressure to prevent airborne migration into finished product cooling corridors.
- 3. Rapid Surface Swabbing & Lateral Flow Device (LFD) Screening: Before any production transition, equipment contact surfaces undergo high-sensitivity LFD swab testing capable of detecting protein residues at levels as low as 2.5 µg/cm².
OEM Production Capability Comparison Matrix
Overview of technical specifications, packaging capabilities, and safety parameters across major product categories.
| Product Category | Primary Ingredients | Gluten Control Standard | Packaging Formats | Certifications |
|---|---|---|---|---|
| Sandwich Biscuits & Crackers | Rice Flour, Tapioca Starch, Cassava | < 5 ppm (R5 ELISA verified) | 300g Box, Flow-Pack, Trays | IFS Food, BRCGS, HACCP |
| Meat Snacks & Jerky | Premium Beef, Soy Sauce (Gluten-Free) | < 10 ppm Dedicated Suite | 20g Single Bag, Bulk Pouch | BRCGS Grade AA, Halal |
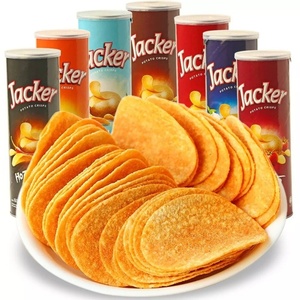
| Extruded Chips & Pellets | Potato Flakes, Corn Starch, Rice Powder | < 5 ppm Air-Locked Hall | 70g Canister, 180g Pillow Pack | ISO 22000, Non-GMO |
| Functional Gummies & Sweets | Pectin, Gelatin, Fruit Concentrates | Naturally Allergen-Free Suite | Bulk Bags, Display Carton, Doypack | Halal Certified, Kosher |
| Seafood Crisp Crackers | Fresh Prawn Meat, Tapioca Powder | Dedicated Crustacean Processing | Bulk Master Carton, Custom Bag | HACCP, MSC Certified |
Future Procurement & Sourcing Trends in Gluten-Free Food Manufacturing (2026–2030)
As the B2B global food trade evolves, procurement managers must align their supply chains with emerging regulatory shifts and shifting consumer preferences. Understanding these macro trends enables buyers to partner with forward-thinking factories capable of delivering future-proof product lines.
1. Shift Towards Functional & Ancient Grain Matrices
Consumers are demanding higher nutritional density from gluten-free snacks. Simple refined starches (such as white rice flour or cornstarch) are rapidly being supplemented or replaced by ancient grains and legumes including quinoa, amaranth, teff, sorghum, and green lentil flour. Modern factories must possess high-shear extrusion and specialized dough-sheeting technologies capable of handling these high-fiber, non-elastic dough matrices without compromising structural integrity or crispness.
2. Clean Label & Ultra-Low Synthetic Additives
Synthetic hydrocolloids and emulsifiers previously used to mimic gluten's binding properties (such as modified food starches and artificial gums) are facing regulatory scrutiny and consumer pushback. The future of OEM gluten-free formulation lies in natural hydrocolloid synergies—utilizing psyllium husk, chia seed mucilage, and enzymatic starch pre-gelatinization to achieve clean-label declarations while maintaining superior texture and extended shelf-life stability.
3. Eco-Friendly Sustainable Flexible Packaging
Regulatory mandates across the European Union and North America are accelerating the adoption of fully recyclable mono-material barrier films (such as PP/PE laminates) and compostable paper-based flexible pouches. Contract manufacturers must equip their automated bagging suites with ultrasonic sealing technologies capable of maintaining modified atmosphere packaging (MAP) seal integrity without melting recyclable barrier films.
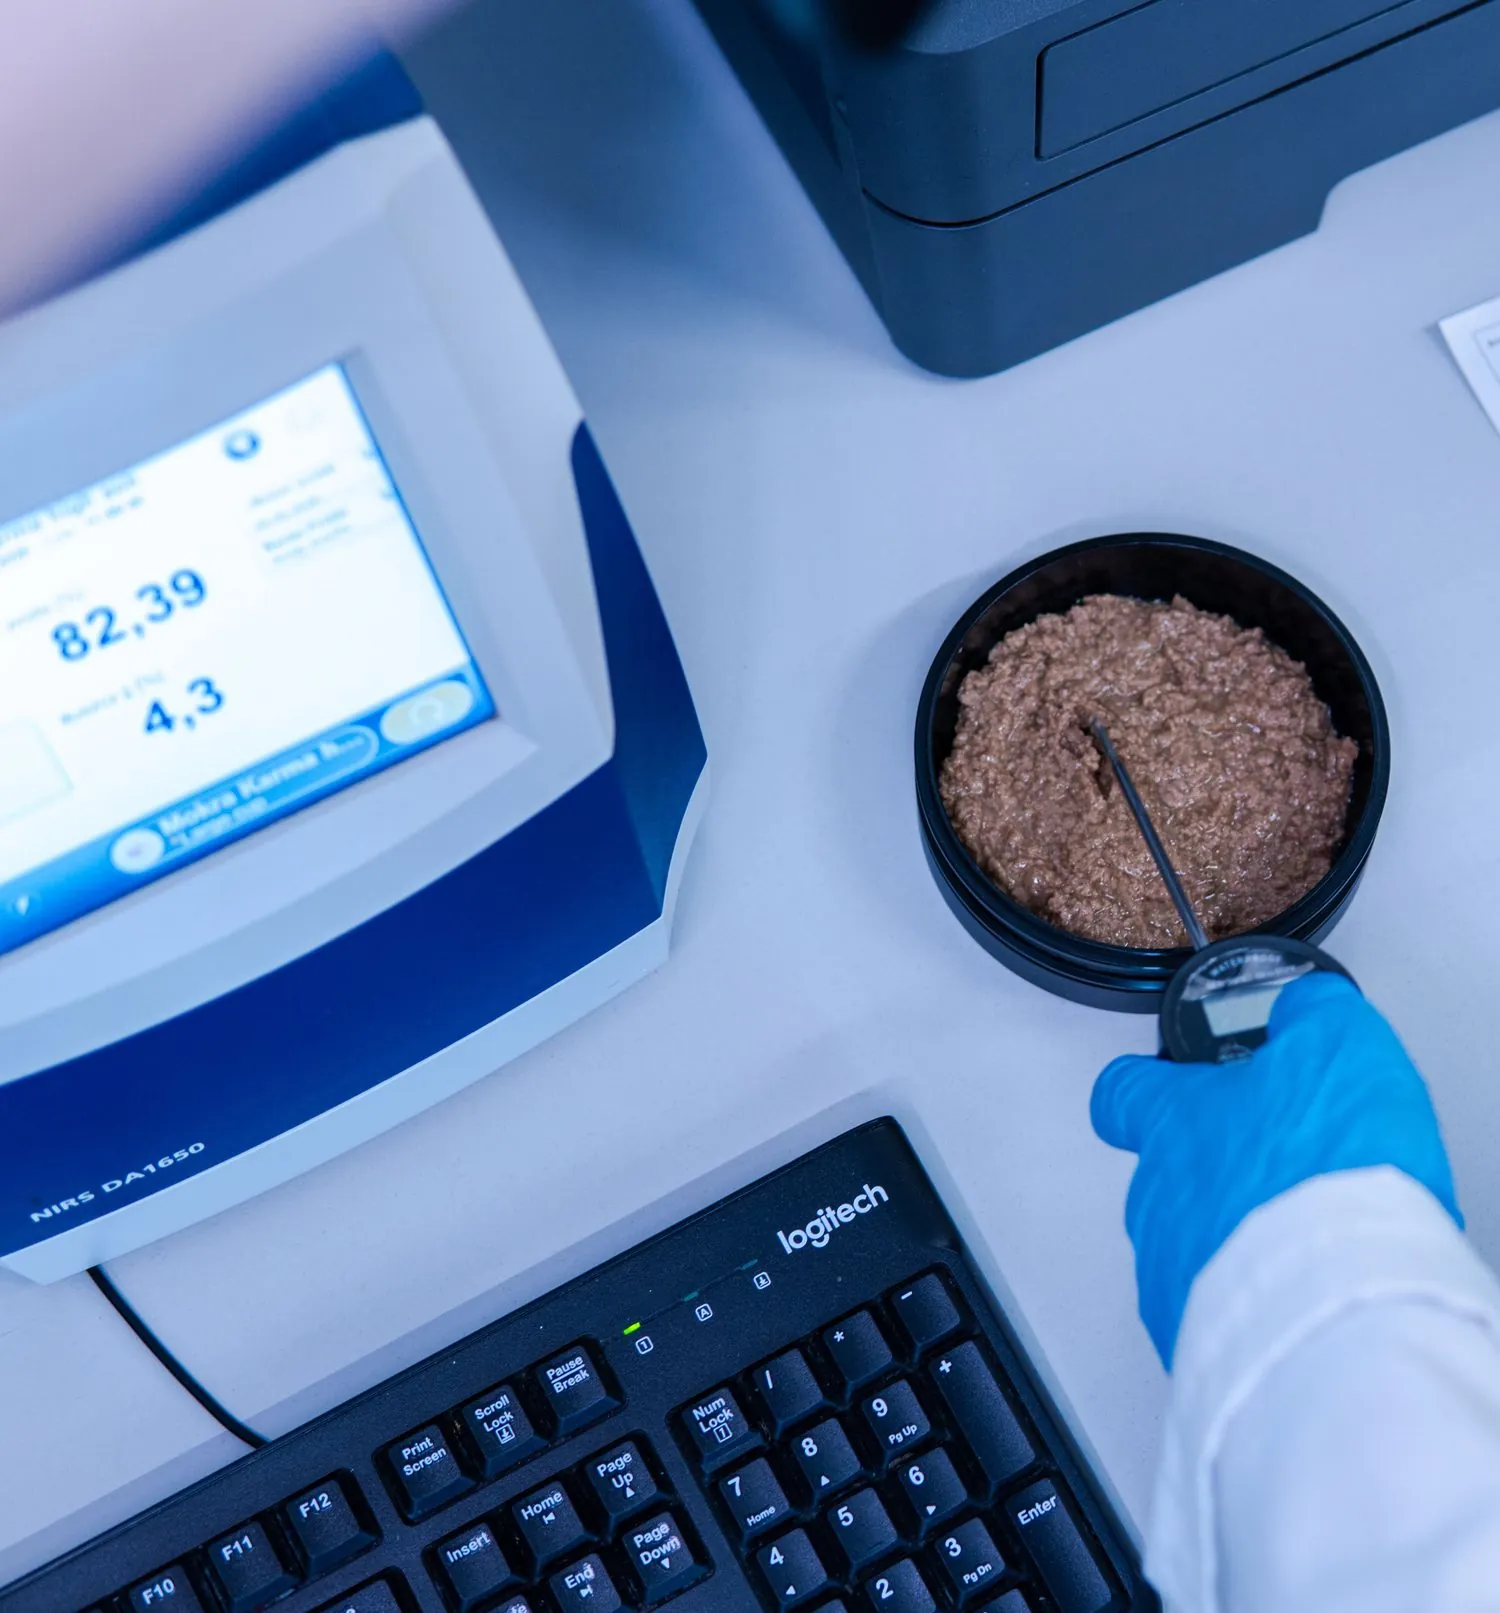
In-House Laboratory Rigor & R&D Expertise
A fundamental requirement of any top-rated gluten-free factory is an on-site, fully equipped testing laboratory. Rather than relying on periodic external third-party testing, our facility conducts real-time raw material screening and continuous in-process quality verification.
Our team of food scientists and quality engineers perform rigorous chemical analysis, moisture determination, water activity (a_w) profiling, and quantitative allergen screenings. This ensures every commercial batch dispatched from our logistics center strictly complies with recipient market regulations across North America, Europe, Asia-Pacific, and the Middle East.
Why Partner with Our Direct OEM Factory Infrastructure?
Building a successful private label snack portfolio requires a manufacturing partner that combines structural scale, flexible minimum order quantities (MOQs), and deep regulatory expertise. Our integrated enterprise offering includes:
- Proprietary Formulation IP Protection: We establish strict non-disclosure agreements (NDAs) to protect customer-owned custom recipes, while offering access to our library of 5,000+ pre-tested, market-ready formulas.
- End-to-End Regulatory Support: Our dedicated export compliance team manages multilingual nutritional labeling, ingredient translation, local food authority registration, and phytosanitary documentation.
- Flexible Contract Packaging Solutions: From micro-dose 10g individual snack packs for airline/hotel hospitality channels to 1250g family-sized bulk cans and shelf-ready retail display cartons (SRP).
- Agile Pilot Line Development: Rapid prototyping capabilities allow clients to execute market testing batches, organoleptic trials, and shelf-life verification protocols prior to full-scale commercial rollouts.
Frequently Asked Questions for B2B Buyers
Direct technical answers regarding factory audits, ordering protocols, allergen validation, and export logsitics.
How does the factory guarantee zero gluten cross-contamination on shared industrial equipment?
What is the standard lead time for private label OEM/ODM production orders?
Can you manufacture gluten-free products according to custom client-supplied recipes?
Which global quality and safety food certifications does your facility maintain?
What are the Minimum Order Quantities (MOQs) for private label snack packaging?
Do you offer export documentation and local market compliance support?
What packaging formats are available to protect moisture-sensitive gluten-free snacks?
Can I request factory sample kits and lab test certificates before placing a commercial order?
Partner with a Trusted Gluten Free Manufacturing Leader
Accelerate your brand's market expansion with our certified OEM/ODM production lines, custom formulation capabilities, and uncompromising allergen safety standards.
Send an Inquiry