High-Demand Export-Ready Snack & Food Formulations
Explore our export-compliant white-label products engineered for international brands, retail chains, and wholesale distributors worldwide.
China's Premier Industrial White Label Infrastructure
Combining state-of-the-art automated manufacturing with rigorous international food safety compliance to deliver unmatched value for global brand owners.
Fully Integrated OEM/ODM Ecosystem
From initial market research, raw ingredient sourcing, and custom formulation engineering to artwork design, primary/secondary co-packing, and global logistics execution. Our unified single-owner process eliminates supply chain friction and dramatically accelerates time-to-market.
Tier-1 Quality Assurance & Certifications
Our manufacturing facilities operate under stringent international standards including IFS Food, BRCGS Grade AA, HACCP, ISO 22000, and Halal Certification. Every production lot undergoes end-to-end batch verification in our in-house microbiological and chemical testing laboratories.
Flexible Packaging & Format Innovation
We support a vast array of packaging formats tailored to regional retail environments: nitrogen-flushed pouch trays, rigid cans, vacuum-sealed flow packs, individual portion packs, display boxes, and eco-friendly recyclable doypacks, ensuring optimal product shelf stability.
Macro Trends Transforming Global White Label Manufacturing
A strategic analysis of the consumer shifts, technological breakthroughs, and macro-economic factors reshaping private label food processing in China and global export markets.
The global contract food manufacturing and private label export industry is undergoing a structural transformation. Driven by heightened consumer scrutiny surrounding nutritional transparency, functional wellness, and environmental footprint, international buyers are re-evaluating their global supply chains. China's manufacturing sector has rapidly evolved from low-cost mass commodity production to high-tech, precision formulation engineering and clean-label co-manufacturing.
1. The Clean-Label Revolution and Nutrient-Dense Formulations
Modern consumers in North America, Europe, and the Asia-Pacific region are demanding shorter, more recognizable ingredient decks. Synthetic preservatives, artificial azo dyes, and hydrogenated fats are being aggressively phased out in favor of natural antioxidants (such as mixed tocopherols and rosemary extracts), plant-based colorants (beetroot, paprika, spirulina extracts), and wholesome real-food bases.
As a leading white label partner, our R&D departments have pioneered high-protein, low-glycemic, and gluten-free snack substrates. Whether developing naturally dried high-protein meat jerky, extruded pulse crisps, or sugar-free pectin-based functional gummies, our processing technology preserves bioactive nutrients while delivering superior organoleptic profiles.
2. Advanced Retort, Extrusion, and Controlled Dehydration Technologies
Product texture and stability without artificial additives rely heavily on modern processing machinery. Key technological shifts include:
- Twin-Screw High-Moisture Extrusion (HMEC): Enables the creation of novel plant-based and high-protein snack matrices with realistic fibrous textures.
- Computer-Controlled Retort Sterilization: Microprocessor-driven steam-air and water-immersion retorts ensure complete commercial sterility for canned, pouch, and jar packaging while minimizing thermal degradation of flavor molecules.
- Low-Temperature Vacuum Drying & Dehydration: Preserves vibrant natural colors, delicate crispiness, and nutritional integrity in sea vegetable, fruit, and seafood snack lines.
3. Sustainable Eco-Friendly Packaging & Regulatory Harmonization
Extended Producer Responsibility (EPR) regulations and corporate ESG mandates are making recyclable and biodegradable packaging a baseline operational requirement for global export. Our manufacturing infrastructure incorporates fully recyclable Mono-PE and Mono-PP barrier films, FSC-certified secondary paperboard packaging, and light-weighted tinplate packaging solutions designed to satisfy stringent EU Directive standards.
Future Sourcing Strategies for International Brand Directors
How forward-thinking procurement executives can leverage China's white label capabilities to optimize unit costs, secure supply chain resiliency, and achieve rapid market scaling.
Navigating geopolitical shifts, tariff fluctuations, and freight dynamics requires a strategic paradigm shift in international OEM/ODM procurement. Sourcing directors are moving away from spot purchasing toward long-term strategic co-manufacturing partnerships that provide technical agility and risk mitigation.
A. Agile Production Scale and Flexible MOQ Structures
Historically, Chinese mega-factories required prohibitively high Minimum Order Quantities (MOQs), creating high inventory barrier risks for mid-market brands. The future of strategic white-label sourcing lies in modular production lines. By deploying high-speed digital packaging setups alongside agile pilot plants, our enterprise allows brand owners to test new consumer flavors, seasonal SKUs, and promotional multipacks with minimal capital risk.
B. End-to-End Digital Batch Traceability & Blockchain Integration
Supply chain visibility is non-negotiable for global retail listing. Advanced B2B exporters now implement complete digital genealogy tracking. Every incoming raw ingredient lot—from high-protein beef cuts to botanical extracts and specialized sweeteners—is logged via barcode and RFID tracking. This data flows through our Enterprise Resource Planning (ERP) system down to the individual finished shipping carton, enabling instantaneous recall capability and complete transparent audit trails for regulatory compliance.
C. Regional Customization and Religious Certification Compliance
Global brand expansion requires strict adherence to localized dietary laws and cultural preferences. A major growth trajectory in white label sourcing involves securing specialized dietary certifications prior to market entry. Our production facility maintains strict segregation protocols to offer fully verified Halal, Kosher, Non-GMO Project Verified, and Organic-certified manufacturing runs, empowering brand owners to seamlessly penetrate Middle Eastern, Southeast Asian, and Western specialty retail sectors.
The 5-Step White Label Onboarding Framework
Brief & Concept Analysis
Product brief evaluation, flavor profile target definition, target market regulatory audit, and cost target alignment.
R&D & Lab Bench Samples
Benchtop formulation engineering, sensory panel testing, analytical nutritional testing, and initial sample dispatch.
Trial Run & Verification
Pilot line manufacturing, packaging line compatibility verification, shelf-life stress testing, and artwork finalization.
Mass Commercial Production
Automated high-speed manufacturing, continuous inline quality monitoring, and secondary automated packaging.
Global Export Release
Customs clearance documentation, phytosanitary/health certificates, COA generation, and optimized freight logistics.
White Label Technical Specifications & Manufacturing Scope
Comprehensive overview of processing capabilities, packaging machinery options, compliance standards, and lead times.
| Product Category | Core Processing Technology | Primary Packaging Formats | Shelf Life Range | Standard Lead Time |
|---|---|---|---|---|
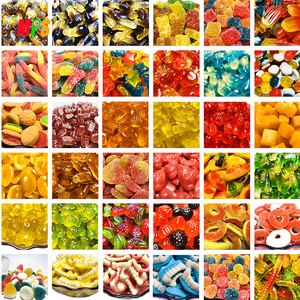
| Confectionery & Gummies | Starch-Mould / Pectin & Gelatin Depositing | Individual Pillow Pack, Doypack, Jar, Display Box | 12 – 24 Months | 30 – 45 Days |
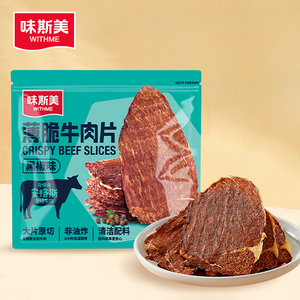
| High-Protein Meat Snacks | Controlled Thermal Dehydration & Retort | Vacuum Nitrogen Pack, Flow Pack, Stand-up Pouch | 9 – 18 Months | 35 – 50 Days |
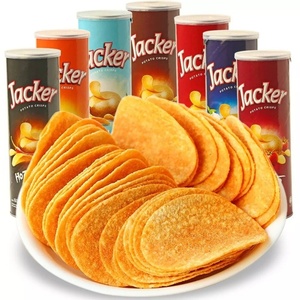
| Crisp Savory & Potato Chips | Continuous Extrusion & Vacuum Frying | Rigid Composite Cans, Foil Bags, Pillow Pouches | 9 – 12 Months | 25 – 40 Days |
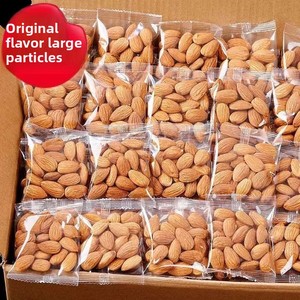
| Nuts & Healthy Seed Packs | Precision Roasting & Nitrogen Gas Flushing | Single-Serve 10g-50g Sachets, Multi-packs, Bulk Bags | 12 Months | 20 – 35 Days |
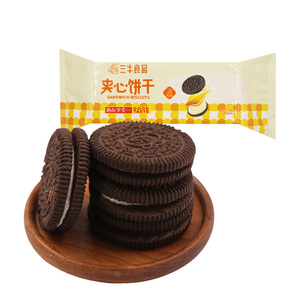
| Bakery & Sandwich Biscuits | Automated Rotary Moulding & High-Capacity Baking | Tray with Flow Wrap, Retail Boxes, Tin Containers | 12 Months | 30 – 45 Days |
| Seafood & Prawn Crackers | Micro-Pellet Puffing & Flavored Coating | Bulk Bags, Nitrogen Filled Pillow Packs, Family Tubs | 10 – 12 Months | 25 – 35 Days |
Frequently Asked Questions for B2B Importers & Brand Owners
Direct answers to common technical, legal, and operational inquiries regarding contract manufacturing in China.
1. What is the typical lead time from initial concept brief to final export shipment?
Our standard production schedule spans 45 to 60 days for newly engineered custom formulations. This includes initial brief review (1–2 days), formulation lab benchwork and sample sign-off (14–21 days), pilot trial verification (7–10 days), mass production and primary packaging (14–21 days), and final export container loading and COA release (3–5 days). For existing turn-key catalog formulations with client artwork, lead times are reduced to 25–35 days.
2. How do you guarantee compliance with FDA, EU, and regional import regulations?
Our regulatory affairs department works directly with your compliance team prior to mass manufacturing. We audit all ingredient decks against target destination market regulations (e.g., FDA CFR Title 21, EU Food Safety Authority directives, GCC Halal standards). Furthermore, we handle all export documentation including Certificate of Analysis (COA), Phytosanitary Certificates, Health Certificates, Certificate of Origin, and complete nutritional panel translation audits.
3. Can you reproduce or re-engineer an existing market product (Benchmarking / Reverse Engineering)?
Yes. Our in-house food technologists and analytical laboratory can perform comprehensive benchmarking analysis on target market products. We evaluate Brix levels, water activity (Aw), moisture content, texture profiles, and nutritional macros to develop an identical or upgraded OEM version optimized for your target cost structure.
4. What non-disclosure and intellectual property (IP) protection measures do you enforce?
Protecting client IP is fundamental to our business model. Before discussing specific recipe formulations or commercial terms, we execute a legally binding Non-Disclosure Agreement (NDA) and Non-Circumvention Agreement. Proprietary client formulations are stored in encrypted recipe management databases accessible only by authorized senior R&D personnel.
5. What are the standard payment terms and shipping options (Incoterms)?
We offer flexible international commercial terms tailored to established importers, including FOB (Free on Board - Qingdao/Ningbo/Shanghai), CIF (Cost, Insurance, and Freight), and DDP (Delivered Duty Paid). Standard payment terms for new white label orders are 30% T/T deposit upon order confirmation and artwork sign-off, with the remaining 70% balance payable against the presentation of the original Bill of Lading (B/L) and inspection certificate.
6. What sustainability options exist for flexible and rigid packaging lines?
We offer full eco-friendly packaging conversions across our primary and secondary packing lines. Options include 100% recyclable mono-layer PE/PP pouches, post-consumer recycled (PCR) plastics, industrially compostable PLA films, and FSC-certified paperboard outer cartons. Our technical team ensures these sustainable materials maintain required oxygen and moisture barrier properties to preserve full shelf life.