Featured OEM Snack & Canned Food Formats
Explore our high-capacity OEM/ODM shelf-stable products engineered with high-barrier packaging, precise retort thermal sterilisation, and clean-label formulations.
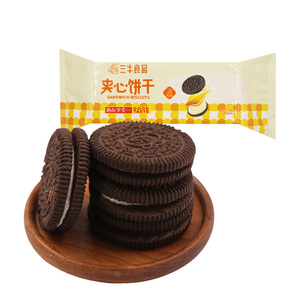
Sanniu Sweet Sandwich Biscuits Box 300g Healthy Snacks Chinese Food Exotic Crackers Biscuit Maker
Send an Inquiry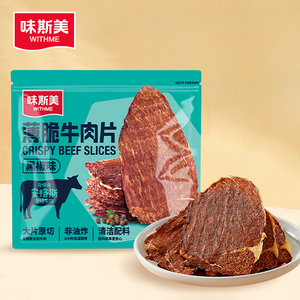
Chinese Spicy Snacks Wholesale 20g Bag individually packaged Black Pepper Flavor High Protein Dry Snacks Beef Jerky for Humans
Send an Inquiry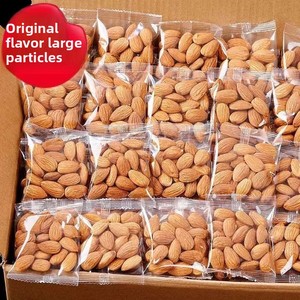
Almond Snacks 10g in Individual Small Packages Original Flavor Nut Snacks New Year Goods Wholesale & Delivery
Send an Inquiry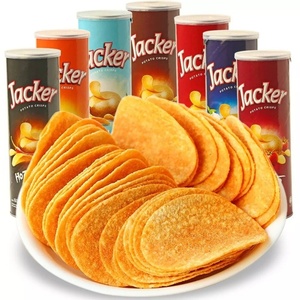
Wholesale Bulk Exotic Chips 70g Tasty Healthy Snack Exotic Snacks 180g Spicy Flavors Potato Chips with Can Package
Send an Inquiry
Wholesale Custom Halal Chinese Bulk Sweet Sour Flavor Jelly Gummy Sweets and Candies
Send an Inquiry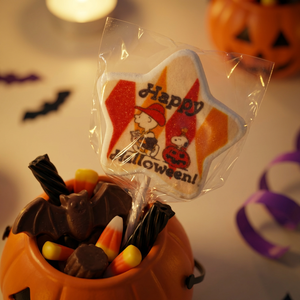
Star Shape Cartoon Character Lollipop Stick 30g x 24pcs Display Box Mixed Fruity Bulk Wholesale Snack
Send an Inquiry
Wholesale Price High Quality Fruity Sweet Cartoon Shape Gummy Candy Halal Certified Snacks MiniCrush
Send an Inquiry
Factory Wholesale Crispy Prawn Crackers Seafood Snacks Customizable Flavors Bulk Packaging Health Snacks for Leisure
Send an InquiryManufacturing Footprint & Operational Metrics
Top 10 Canned Food Factories: Global Capabilities Analysis
To navigate the complex global contract manufacturing landscape, food brand owners and B2B procurement heads require transparent operational metrics. Below is an executive comparison of leading thermal-processing and canning facilities worldwide.
| Factory / Manufacturer | Primary Specialization | Key Certifications | Retort & Packaging Options | Daily Production Yield |
|---|---|---|---|---|
| Global Pet's Food Sp. z o.o. (Poland Facility) | Wet Cat/Dog Canned Food, Retort Pouches, Meaty Chews | IFS Food, BRCGS, HACCP, ASC, MSC | Cans (85g-1250g), Alupack (85g-500g), Doypacks, Jars | 450,000 Units / Day |
| Conagra Brands OEM Facility (USA) | Commercial Ready-Meals, Vegetables, Soups | SQF Level 3, USDA Organic, FDA Registered | Tinplate Cans, Composite Containers, Trays | 1,200,000 Units / Day |
| Thai Union Group Packaging Hub (Thailand) | Seafood Canned Goods, Tuna, Pet Nutrition Cans | BRCGS, IFS, ISO 22000, MSC Chain of Custody | Easy-Open Aluminium Cans, Retort Pouches | 2,500,000 Units / Day |
| Bolton Food Production Facilities (Italy/Spain) | Mediterranean Canned Fish, Meat Retort Jars | IFS Food, BRCGS, Dolphin Safe, ISO 14001 | Aluminium Cans, High-Barrier Glass Jars | 850,000 Units / Day |
| COFCO Sugar & Canned Goods Mfg (China) | Canned Fruits, Tomato Pastes, Agricultural Produce | HACCP, ISO 9001, BRCGS, Halal, Kosher | Bulk Tinplate Cans, Institutional Packaging | 1,800,000 Units / Day |
| Del Monte Foods Manufacturing (USA) | Preserved Vegetables, Fruit Retort Cups, Broths | SQF Edition 9, Non-GMO Project Verified | BPA-NI Cans, Plastic Fruit Cups, Pouches | 1,500,000 Units / Day |
| Kraft Heinz OEM Network (Global) | Canned Sauces, Baked Beans, Retort Soups | GFSI Benchmarked, FSSC 22000 | Steel Cans, Tetra Recart Cartons | 3,000,000 Units / Day |
| Campbell Soup Supply Chain (North America) | Condensed Soups, Broths, Liquid Meals | SQF Level 3, USDA High Hazard Safety | Pull-Tab Cans, Microwaveable Bowls | 2,000,000 Units / Day |
| Century Pacific Food (Philippines) | Canned Meat (Corned Beef), Tuna, Dairy Liquids | HACCP, Halal Certified, BRCGS | Two-Piece & Three-Piece Can Formats | 1,100,000 Units / Day |
| Nisshin Oillio & Food Processing (Japan) | Functional Retort Packs, High-Barrier Edible Cans | FSSC 22000, Japanese Agricultural Standard (JAS) | Soft-Pouch Retort, Precision Aluminium Cans | 600,000 Units / Day |
Why Leading Retail Brands Partner with Our Manufacturing Hub
Operating out of our modern facility in Koźmin Wielkopolski, Poland, our organization brings together over 250 food technology experts, mechanical engineers, and quality assurance officers. We operate an integrated end-to-end processing ecosystem that eliminates intermediary friction, ensuring unmatched batch-to-batch consistency.
- Fully Automated Retort & Sterilization Steam Loops: Computer-controlled F0 lethality calculation guarantees commercial sterility without degrading vital nutrients or product texture.
- Rigorous In-House QC Laboratory: Every raw material delivery undergoes physical, chemical, and microbiological screening prior to batch formulation.
- IFS Food v8 & BRCGS Grade A Certification: Compliant with the highest international standards required by tier-1 global supermarket networks and fast-tracked listing processes.
- End-to-End Packaging Versatility: Direct filling line integration for 85g-1250g metal cans, flexible aluminum pouches, standing doypacks, and wide-mouth glass jars.
- ASC & MSC Certified Sustainable Sourcing: Chain-of-custody documentation verifying that ocean marine ingredients are harvested responsibly.
Future Procurement Trends in Canned & Preserved Foods
As consumer demand shifts toward sustainable packaging, clean-label preservatives, and novel proteins, B2B procurement managers must align with contract factories engineered for next-generation manufacturing.
Transition to BPA-NI & Recyclable Metals
Regulatory pressures in North America and the EU are expediting the complete phase-out of Bisphenol-A (BPA). Advanced factories are shifting toward BPA-Non-Intent (BPA-NI) acrylic and organosol lacquers alongside infinitely recyclable thin-gauge steel and aluminum alloys.
Clean-Label & Minimalist Processing
Modern buyers demand shelf-stable foods free from artificial binders, excessive sodium, and chemical emulsifiers. Retort processing techniques utilize gentle agitation cookers to achieve commercial sterilization while maintaining high nutritional density.
Flexible Doypack & Alupack Surge
While traditional round tin cans remain a backbone of institutional supply, lightweight stand-up pouches and aluminum trays offer up to 40% reductions in shipping volume and carbon footprint, driving immense growth in retail snacking and pet nutrition segments.
Single-Origin & Novel Proteins
Procurement for human wet food and pet nutrition is increasingly prioritizing hypoallergenic single-protein sources (e.g., wild-caught salmon, duck, venison). Transparency in raw material origins allows brands to command premium price margins.
Decentralized Co-Packing Networks
To mitigate global logistics disruptions, multinational brand owners are decentralizing production by establishing contract manufacturing hubs within Europe and regional trade zones, reducing shipping lead times from months to days.
Smart Traceability & Digital Auditing
Blockchain-enabled supply chain verification and instant QR-code batch tracking are becoming mandatory for supermarket listing qualification, providing real-time data from raw material harvest to retail shelf placement.
Engineering Excellence: Thermal Retort & Hermetic Sealing
Commercial canned food production relies on the science of thermal penetration, barrier chemistry, and airtight mechanical seams. Our processing lines integrate state-of-the-art automation to ensure absolute sterility and prolonged shelf stability.
1. Computer-Controlled Autoclave Retorts
Using water-spray steam autoclaves with overpressure control, heat distribution is uniform across all container geometry. Real-time temperature sensors record lethal rate values ($F_0 \ge 3.0$), killing heat-resistant spores such as Clostridium botulinum while preserving delicate natural flavors.
2. Double-Seam Integrity Inspection
Mechanical hermetic sealing of 2-piece and 3-piece cans undergoes continuous optical seam inspection. Parameters such as seam length, overlap, countersink depth, and body hook thickness are non-destructively verified via high-resolution X-ray vision systems.
3. High-Barrier Multi-Layer Laminates
For flexible retorting (pouches and doypacks), our lines utilize high-barrier CPP (Cast Polypropylene) combined with aluminum foil or SiO2 barrier films. This structure prevents oxygen permeation ($< 0.1 \text{ cc/m}^2/\text{day}$) and moisture transmission, granting up to 36 months of ambient shelf life.
Frequently Asked Questions by OEM Procurement Managers
Key answers regarding contract manufacturing lead times, recipe formulation, packaging customization, and export logistics.
The standard turnaround time is 45 to 60 days from approved product specification. This timeline covers: initial recipe brief & validation (1-2 days), R&D recipe development (14-21 days), pilot trial runs & thermal penetration testing (7-10 days), full production series (14-21 days), and final dispatch documentation clearance (2-5 days).
Our facility holds audited and active certifications for IFS Food (International Featured Standards), BRCGS Global Standard for Food Safety, HACCP, as well as ASC (Aquaculture Stewardship Council) and MSC (Marine Stewardship Council) chain-of-custody credentials for responsibly harvested seafood ingredients.
Yes. We regularly perform contract manufacturing based on customer-provided recipes. Prior to line trial runs, our food technology team verifies technical feasibility, nutritional target compliance (such as FEDIAF or AAFCO guidelines), and raw material stability under retort sterilization conditions. A non-disclosure agreement (NDA) is executed prior to recipe exchange.
We support a broad spectrum of formats: flexible alupack pouches (85g to 500g), metal cans (85g to 1250g with easy-open or standard ends), pâté trays (100g to 300g), glass jars (100g to 150g), and stand-up doypacks. Eco-friendly recyclable multi-layer laminates are also available.
Quality control operates on four distinct levels: raw material intake testing, automated in-line critical control point (CCP) monitoring during mixing and retorting, laboratory release testing for commercial sterility, and automated optical vision checks for container seal integrity and packaging labeling.
Yes. Our regulatory affairs department assists in creating multi-language label layouts, nutritional declaration panels, veterinary export certificates, certificate of analysis (COA), and customs documentation for EU, North American, Asian, and Middle Eastern import standard compliance.
Ready to Develop Your Next Canned Food Line?
Partner with an audited, high-capacity European contract manufacturer. Contact our OEM sales engineering team for recipe formulations, technical specifications, and custom quote estimations within 24 hours.