Featured Food & Snack Bulk Packaging Solutions
Explore our top-tier OEM & wholesale bulk packaged products engineered for maximum shelf stability, export compliance, and sensory preservation.
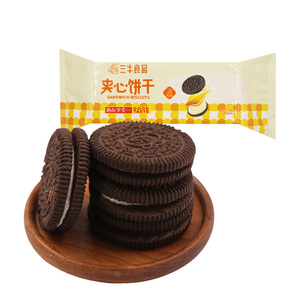
Sanniu Sweet Sandwich Biscuits Box 300g Healthy Snacks Chinese Food Exotic Crackers Biscuit Maker
Contact Us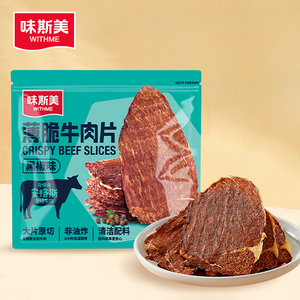
Chinese Spicy Snacks Wholesale 20g Bag individually packaged Black Pepper Flavor High Protein Dry Snacks Beef Jerky for Humans
Contact Us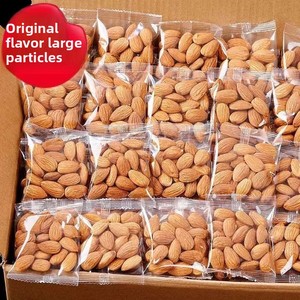
Almond Snacks 10g in Individual Small Packages Original Flavor Nut Snacks New Year Goods Wholesale & Delivery
Contact Us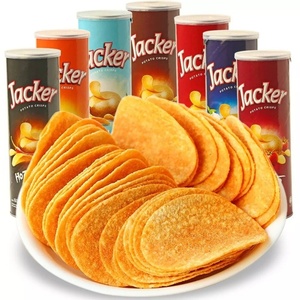
Wholesale Bulk Exotic Chips 70g Tasty Healthy Snack Exotic Snacks 180g Spicy Flavors Potato Chips with Can Package
Contact Us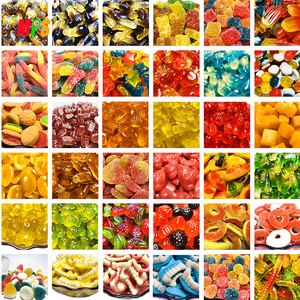
Wholesale Custom Halal Chinese Bulk Sweet Sour Flavor Jelly Gummy Sweets and Candies
Contact Us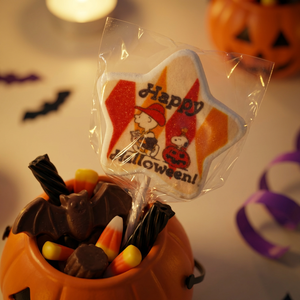
Star Shape Cartoon Character Lollipop Stick 30g x 24pcs Display Box Mixed Fruity Bulk Wholesale Snack
Contact Us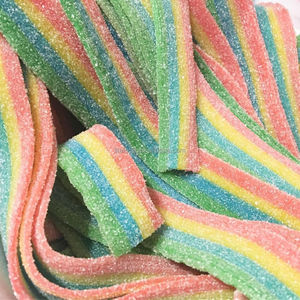
Wholesale Price High Quality Fruity Sweet Cartoon Shape Gummy Candy Halal Certified Snacks MiniCrush
Contact Us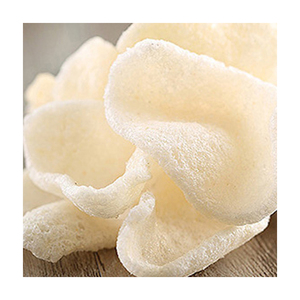
Factory Wholesale Crispy Prawn Crackers Seafood Snacks Customizable Flavors Bulk Packaging Health Snacks for Leisure
Contact UsState of Global Bulk Packaging: Engineering Resilience, Barrier Integrity & Market Growth
In the contemporary FMCG, food processing, and specialty retail sectors, bulk packaging has evolved from a passive containment vector into a critical strategic asset. As global supply chains face heightened volatility, stringent environmental mandates, and demanding quality compliance standards, international procurement officers are recalibrating their sourcing criteria. Choosing the optimal manufacturing partner in China—the epicenter of global advanced manufacturing—requires a granular understanding of material science, barrier performance, automated contract packing, and international regulatory frameworks such as IFS Food, BRCGS, HACCP, and ISO 22000.
Bulk packaging for food and consumable products encompasses a broad spectrum of engineered flexible laminates, multi-layer rigid structures, modified atmosphere packaging (MAP), and shelf-ready retail display units. The primary objective is twofold: preserving product integrity across extended transit cycles and reducing operational landed costs per unit through volume optimization. As modern consumer preferences shift toward single-serve individually wrapped portions inside secondary bulk packaging, manufacturers must operate high-speed, automated cleanroom packaging environments capable of handling complex micro-dosing and moisture-sensitive snacks.
Strategic Sourcing Insight: Advanced multi-layer extrusion co-polymer films (featuring EVOH and metallized PET barriers) provide up to a 99.8% reduction in oxygen and moisture ingress compared to traditional single-layer PE structures, directly extending product shelf life up to 24 months without synthetic preservatives.
As a leading China bulk packaging manufacturer and supplier, our enterprise combines state-of-the-art technological infrastructure with rigorous quality assurance protocols. By centralizing technical design, raw material synthesis, high-definition flexographic printing, lamination, and automated contract packing under a single quality management system, we eliminate supply chain friction and deliver quantifiable information gain for corporate procurement teams.
Core Manufacturing Advantages: Technical Infrastructure & Quality Assurance
Our production ecosystem is built around precision engineering, high-throughput efficiency, and total traceable quality control. Operating across 18 specialized high-speed production and packaging lines within Class 100,000 cleanroom environments, our facility handles diverse bulk packaging formats ranging from individual small sachets (10g–30g) to heavy-duty bulk bag containers and rigid cans.
High-Barrier Laminates
Multi-layer co-extrusion incorporating AL, VMPET, EVOH, and bio-PE for superior Oxygen Transmission Rate (OTR) and Water Vapor Transmission Rate (WVTR) protection.
Global Audited Compliance
Certified to IFS Food, BRCGS Global Standard for Food Safety (Issue 9), HACCP, and ISO 22000. Full batch traceability from raw material intake to dispatch.
Rapid OEM/ODM Development
In-house R&D laboratory equipped with gas chromatography and tensile testing. Full turn-key product launch cycles completed within 45 to 60 days.
In-House Quality Control Laboratory & Batch Traceability
Quality reliability is non-negotiable when dealing with bulk food and industrial packaging. Every production batch undergoes a four-stage quality verification protocol: raw resin purity testing, continuous online optical thickness gauging during extrusion, hermetic seal integrity testing under dynamic pressure, and post-packaging microbiological screening. This technical rigor ensures zero seal failure during long-haul sea freight and extreme environmental transitions.
Technical Capability Matrix: Bulk Packaging Materials & Formats
Below is a comparative breakdown of key packaging substrates, performance specifications, and target application suitability designed to assist procurement directors in material selection.
| Packaging Format | Material Composition | Barrier Metrics (OTR / WVTR) | Key Application Features | Typical Lead Time |
|---|---|---|---|---|
| Alupack Pouch / Sachet | PET / AL / LLDPE (High Barrier) | OTR < 0.1 cc/m²/day WVTR < 0.1 g/m²/day |
Lightproof, hermetic seal, individual snack wraps (10g–50g), vacuum sealing. | 30 – 45 Days |
| Recyclable Doypack | Mono-Material PE (MDO-PE / PE) | OTR < 2.0 cc/m²/day WVTR < 1.5 g/m²/day |
100% recyclable, clear window options, press-to-close zippers, sustainable retail. | 35 – 45 Days |
| Rigid Can / Composite Tube | Tinplate / Kraft Paper / Foil Liner | Total Light & Gas Ingress Protection | Crush-proof protection for fragile chips, nuts, extruded snacks, display ready. | 40 – 50 Days |
| Bulk Corrugated Master Carton | Double-Wall Heavy Duty Flute (EB/BC) | Bursting Strength > 1800 kPa | Export transit protection, moisture-resistant coating, dynamic stacking endurance. | 15 – 25 Days |
Global Sourcing & Future Industry Trends (2026–2030)
The global bulk packaging sector is undergoing a paradigm shift driven by three primary forces: stringent sustainability mandates (e.g., EU Packaging and Packaging Waste Regulation - PPWR), rapid adoption of industrial packaging automation, and consumer demand for single-origin and exotic snack bulk options.
1. Transition to Mono-Material Sustainable Laminates
Traditional multi-layer flexible packaging combining disparate polymers (such as PET glued to PE or Foil) creates recycling bottlenecks. Strategic procurement is rapidly gravitating toward Mono-Material structures—specifically MDO-PE (Machine Direction Oriented Polyethylene) laminated with PE resins. These structures maintain structural rigidity, high clarity, and print resolution while delivering 100% circular recyclability within established curbside waste streams.
2. Active Packaging & Gas Flushing (MAP) Integration
To combat food degradation without chemical additives, advanced bulk packaging now integrates active barrier elements, including oxygen scavengers and ethylene absorbers, alongside Modified Atmosphere Packaging (MAP) technology. By flushing nitrogen (N₂) or carbon dioxide (CO₂) into secondary bulk packaging during high-speed automated filling, oxidation and rancidity in lipid-heavy products (such as roasted almonds, spicy beef jerky, and fried potato chips) are virtually eliminated.
3. Smart Logistics & RFID Bulk Tracking
Bulk master cases and palette-level packaging are increasingly integrated with digital intelligence. Embedded QR codes, serial barcodes, and printable RFID tags enable real-time warehouse location tracking, cold-chain temperature logging, and automated anti-counterfeiting verification across transit routes from China manufacturing ports to North American and European distribution centers.
Product Development Trends & Customized OEM/ODM Workflow
Building a successful private label or bulk packaging program requires seamless collaboration between brand owners and manufacturing partners. Our OEM/ODM workflow is structured to minimize technical risk and accelerate time-to-market:
Brief & Technical Scoping
Initial evaluation of product physical characteristics, moisture sensitivity, target shelf life, and regional market compliance requirements.
Formulation & Trial Prototyping
Material substrate selection, tensile and barrier testing, custom die-cut mold creation, and graphic color management (up to 10-color flexo/rotogravure).
Pilot Run & Mass Dispatch
Controlled pilot production batch, hermetic seal verification, stress testing, followed by full-scale automated packaging, palletization, and export shipment.
Whether you require customized shape lollipops in retail display boxes, nitrogen-flushed spicy meat snack sachets, or certified Halal gummy sweet bulk packs, our engineering team optimizes structural packaging thickness to reduce resin usage while enhancing puncture resistance during transport.
Frequently Asked Questions (FAQ) for Global Buyers
Partner with China's Premier Bulk Packaging Manufacturer
Elevate your brand's market competitiveness with high-barrier, sustainable, and custom-engineered packaging solutions. Contact our engineering team today for technical consultation and instant factory quotes.
Contact Us