Featured Dehydrated & Specialty Product Lines
High-capacity export manufacturing under strict IFS Food, BRCGS, and HACCP compliance. Fully customizable recipes, retail packaging, and private label solutions.
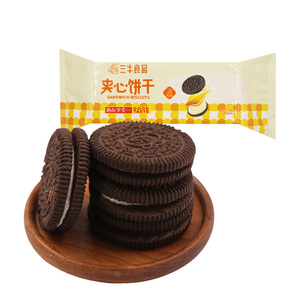
Sanniu Sweet Sandwich Biscuits Box 300g Healthy Snacks Chinese Food Exotic Crackers Biscuit Maker
- Low-temperature baked crust
- Custom sandwich cream filling
- ISO / HACCP Certified Line
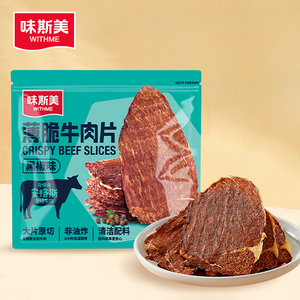
Chinese Spicy Snacks Wholesale 20g Bag individually packaged Black Pepper Flavor High Protein Dry Snacks Beef Jerky for Humans
- Controlled air-dried beef strips
- High protein / Nitrogen flushed
- Export grade single pouch
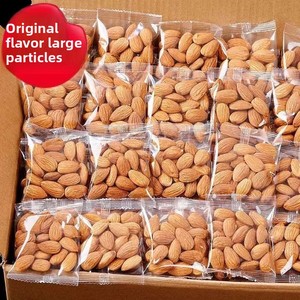
Almond Snacks 10g in Individual Small Packages Original Flavor Nut Snacks New Year Goods Wholesale & Delivery
- Gentle heat-dehydrated nuts
- Preserved natural oils & crunch
- Clean-label preservative free
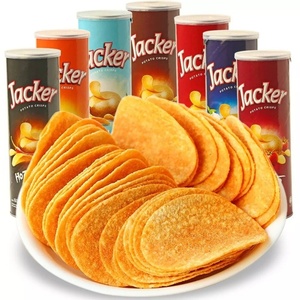
Wholesale Bulk Exotic Chips 70g Tasty Healthy Snack Exotic Snacks 180g Spicy Flavors Potato Chips with Can Package
- Low-oil vacuum air crisping
- Sealed canister moisture barrier
- Custom seasoning formulation
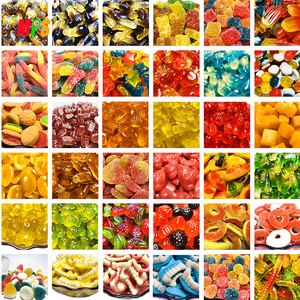
Wholesale Custom Halal Chinese Bulk Sweet Sour Flavor Jelly Gummy Sweets and Candies
- Halal Certified Facility
- Air-conditioned drying rooms
- Bulk & OEM brand formats
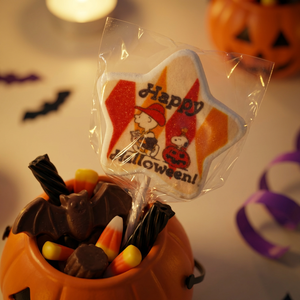
Star Shape Cartoon Character Lollipop Stick 30g x 24pcs Display Box Mixed Fruity Bulk Wholesale Snack
- Precision continuous molding
- Shelf-ready display box packing
- Custom color & fruity flavors
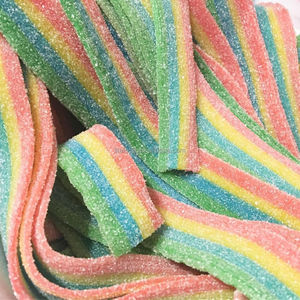
Wholesale Price High Quality Fruity Sweet Cartoon Shape Gummy Candy Halal Certified Snacks MiniCrush
- Controlled moisture extraction
- BRCGS & Halal compliance
- High clarity pectin/gelatin base
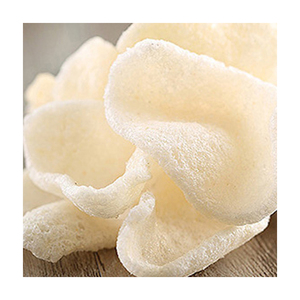
Factory Wholesale Crispy Prawn Crackers Seafood Snacks Customizable Flavors Bulk Packaging Health Snacks for Leisure
- ASC / MSC seafood options
- Rapid thermal crisping tech
- Bulk export palletized loading
Air-Drying Manufacturing Technology in China: Industrial Overview
An authoritative evaluation of thermal dynamics, water activity ($a_w$) control, nutritional degradation mitigation, and regulatory compliance for modern food and pet treat manufacturers.
Biochemical Advantages of Controlled Dehydration
Air drying (controlled thermal dehydration) has evolved from traditional sun-curing into a precision-engineered industrial process. Unlike high-temperature extrusion or conventional frying, modern heat-pump and humidity-controlled air-drying systems operate at low-to-medium thermal bands (45°C to 70°C). This preserves critical bio-available nutrients, structural proteins, natural colorants, and volatile flavor compounds.
From a microbial safety standpoint, the goal of leading Chinese dehydration factories is reducing Water Activity ($a_w$) below 0.60. At this thermodynamic threshold, pathogenic bacterial growth (including Salmonella spp., Listeria monocytogenes, and Escherichia coli) as well as mold spores are entirely halted without requiring harsh chemical preservatives.
Furthermore, precision air drying prevents excessive Maillard reactions (uncontrolled caramelization and protein damage), yielding a clean-label product with superior rehydration rates, texture stability, and extended shelf life (up to 24 months in multi-layer barrier packaging).
Key Manufacturing Metrics
Our strategic manufacturing facilities combine advanced European processing standards with China’s robust industrial scale.
Industrial Processing Technology Comparison
Understanding the technical trade-offs between air drying, freeze drying, and thermal extrusion for global brand owners and procurement decision-makers.
| Preservation Method | Operating Temperature Range | Final Water Activity ($a_w$) | Nutrient Retention Ratio | Cost Efficiency (Capex/Opex) | Optimal Product Categories |
|---|---|---|---|---|---|
| Heat-Pump Air Drying | 40°C – 65°C | 0.45 – 0.58 | 88% – 94% | High Efficiency / Medium Opex | Meat Jerky, Fruit Strips, Functional Treats, Seafood Crackers |
| Freeze Drying (Lyophilization) | -40°C – +30°C (Sublimation) | 0.20 – 0.35 | 95% – 98% | Low Efficiency / Very High Capex | High-Value Raw Meat Nuggets, Bioactive Ingredients, Specialty Fruits |
| Thermal Extrusion | 110°C – 160°C | 0.55 – 0.65 | 60% – 75% | Very High Volume / Low Unit Cost | Standard Kibble, Puffed Snacks, Expanded Grains |
| Vacuum Microwave Drying | 35°C – 55°C | 0.30 – 0.50 | 90% – 95% | Medium Volume / High Energy Efficiency | Quick-Rehydrating Soups, Heat-Sensitive Herbs, Crisp Vegetable Chips |
Why Source Air-Dried Products from Top Chinese Manufacturers?
Combining end-to-end supply chain integration, rigorous quality control laboratories, and rapid customized batch production.
In-House R&D & Formulation
Over 5,000 validated formulations across human leisure snacks, functional nutritional bites, and premium pet diets. Our technical teams work directly under Non-Disclosure Agreements (NDAs) to engineer proprietary flavor profiles, custom shapes, and precise macro-nutritional ratios.
Global Safety Certifications
Production facilities operate in strict accordance with IFS Food Standard, BRCGS (Global Standard for Food Safety), HACCP, ASC, and MSC Chain of Custody. Every batch comes with complete Certificate of Analysis (COA) documents and full forward/backward supply chain traceability.
Automated Dehydration Lines
Utilizing multi-zone continuous belt dehydrators equipped with real-time temperature and humidity sensors. Automated moisture balancing ensures zero hot-spots, uniform texture, consistent sensory profile, and reduced carbon emissions per metric ton produced.
Flexible Private Label Packaging
Complete co-packing and packaging integration: from recyclable mono-material aluminum-pack pouches, stand-up doypacks, gas-flushed flow packs, to shelf-ready display cartons and metal canisters with gas-barrier protection.
Seamless Global Export Compliance
Extensive experience navigating FDA registrations, EU import regulations, customs documentation, sanitary certificates, and country-specific labeling compliance for North America, Europe, Southeast Asia, and the Middle East.
Cost Optimization & Supply Resilience
Direct bulk sourcing from raw material origins coupled with optimized industrial heat recovery systems enables competitive volume pricing without compromising ingredient integrity or microbial safety standards.
Future Procurement & Technology Trends (2025–2030)
Emerging market dynamics shaping product development, sourcing decisions, and brand positioning in global markets.
1. The Clean-Label & Single-Ingredient Movement
Consumers across Western and Asian markets are demanding zero-additive products. In response, air-dried food manufacturers in China are moving toward single-ingredient dried meats, whole-fruit strips, and minimalist formulations that rely purely on physical water extraction ($a_w \le 0.55$) rather than artificial preservatives, sodium metabisulfite, or synthetic antioxidants.
2. Nutraceutical & Functional Infusion
Dehydration serves as an optimal vehicle for delicate functional ingredients. Modern production lines incorporate cold-infusion or gentle spray coating of prebiotics, probiotics, postbiotics, Omega-3 fatty acids, glucosamine, and botanical extracts post-drying to prevent thermal degradation.
3. Eco-Friendly & High-Barrier Packaging Solutions
With global ESG mandates expanding, procurement leaders are prioritizing recyclable mono-material PE/PP pouches and bio-based barrier films. Advanced Chinese factories now offer heat-resistant, low Water Vapor Transmission Rate (WVTR) recyclable materials that maintain full shelf life while meeting EU recyclability directives.
4. Multi-Stage Heat Pump & Microwave Integration
Next-generation factory lines utilize hybrid drying systems. By combining dehumidified cold-air drying in the initial high-moisture phase with vacuum-microwave drying in the final stage, factories achieve up to 40% reduction in processing time while preserving natural cell wall integrity and crunch.
5. Blockchain Traceability & Sustainable Sourcing
B2B buyers are demanding fully audited supply chains. Certification schemes such as ASC (Aquaculture Stewardship Council) and MSC (Marine Stewardship Council) for seafood snacks, alongside sustainable farm verification for beef and poultry, have become critical qualifications for tier-1 retail placement.
6. Low-Carbon Industrial Dehydration
Energy recovery heat exchangers and solar-assisted drying pre-heaters are drastically reducing the energy footprint of dehydration plants, helping international brand owners meet Scope 3 emissions reduction targets.
5-Stage Contract Manufacturing Lifecycle
From initial brief to international container dispatch—how leading Chinese suppliers execute turnkey private label projects in 45 to 60 days.
Technical Brief & NDA
Product brief submission, target market regulatory review, ingredient specification alignment, and mutual NDA execution (1–2 Days).
R&D & Benchtop Sampling
Recipe optimization, sensory evaluation, preliminary moisture testing, color matching, and prototype sample dispatch for client sign-off (14–21 Days).
Pilot Run & Validation
Factory pilot trial run, accelerated shelf-life validation, packaging thermal sealing checks, and microbial challenge testing (7–10 Days).
Commercial Production
Raw material intake inspection, continuous air drying under HACCP monitoring, automated packaging, nitrogen flushing, and metal detection (14–21 Days).
Quality Release & Export
Final COA lab sign-off, export customs documentation preparation, palletization, container loading, and logistics dispatch (2–5 Days).
B2B Procurement & Manufacturing FAQ
Answers to common operational, technical, and regulatory questions from international sourcing teams and brand owners.
What is the standard lead time for private label air-dried food manufacturing in China?
Standard turnaround time ranges from 45 to 60 calendar days for newly developed formulations. This includes initial brief analysis and consultation (1–2 days), recipe and sample formulation (14–21 days), pilot run verification (7–10 days), full mass production (14–21 days), and export dispatch (2–5 days). Repeat order lead times are typically compressed to 20–30 days once packaging artworks and specifications are standardized.
What food safety and quality certifications are required for international export?
Tier-1 Chinese air-drying facilities hold global food safety management certifications including IFS Food (International Featured Standards), BRCGS (British Retail Consortium Global Standard - Grade A/AA), and HACCP. For seafood-based products, ASC (Aquaculture Stewardship Council) and MSC (Marine Stewardship Council) chain-of-custody certifications ensure compliance with EU, US FDA, and Australian DAFF import regulations.
Can your factory manufacture according to custom recipes provided by brand owners?
Yes. OEM contract manufacturing based on customer-supplied formulations is a core capability. Prior to production, an NDA (Non-Disclosure Agreement) is executed. Technical teams review the recipe's thermal feasibility, moisture targets, natural preservative balance, and regulatory compliance for your target market. Adjustments are recommended only to optimize processing yield or extend shelf life without altering core brand attributes.
How is water activity ($a_w$) verified to ensure microbial stability?
Water activity is measured during production using calibrated chilled-mirror dewpoint water activity meters. For air-dried meat, fruit, and snack products, the target $a_w$ is strictly maintained between 0.45 and 0.58. Combined with automated multi-stage temperature logging during the dehydration cycle, this guarantees that moisture levels remain well below the biological growth threshold for pathogenic micro-organisms.
What are the typical Minimum Order Quantities (MOQs) for custom packaging?
MOQs depend heavily on the packaging format selected. For custom-printed stand-up pouches or doypacks with rotogravure or digital printing, MOQs generally start at 10,000 to 20,000 units per SKU. Bulk corrugated export master cartons or plain unprinted pouches with custom adhesive labels can accommodate lower trial order volumes (starting at 500 kg to 1,000 kg of finished product).
What export documentation is provided for clearance in North America and Europe?
A complete export documentation package is provided with every shipment, including Commercial Invoice, Packing List, Bill of Lading (B/L), Certificate of Origin (CO / Form A / Form E), Health & Sanitary Certificate issued by CIQ / Customs, Batch Certificate of Analysis (COA), and heavy metal/microbiology screening reports from accredited third-party laboratories (e.g., SGS, Eurofins).
How does low-temperature air drying compare to freeze drying in terms of cost and quality?
Air drying offers approximately 40% to 60% lower manufacturing energy costs compared to lyophilization (freeze drying) while delivering superior structural density and chewy/crispy textures desirable in meat jerky, crackers, and fruits. While freeze drying excels at maintaining exact 3D shape and extreme low weight, modern heat-pump air drying delivers 88%+ nutrient retention at a significantly more competitive price point for mass retail distribution.
Partner with China's Leading Air-Dried Food Manufacturers
Whether expanding your existing product line or launching a custom private label brand, our technical team provides end-to-end support within 24 hours.
Inquire Now